Warehouse Automation
Robot Charging Infrastructure: Battery Strategy, Opportunity Charging, and Floor Space Planning
Sep 12, 2026 · 14 min read · Robotech Pros
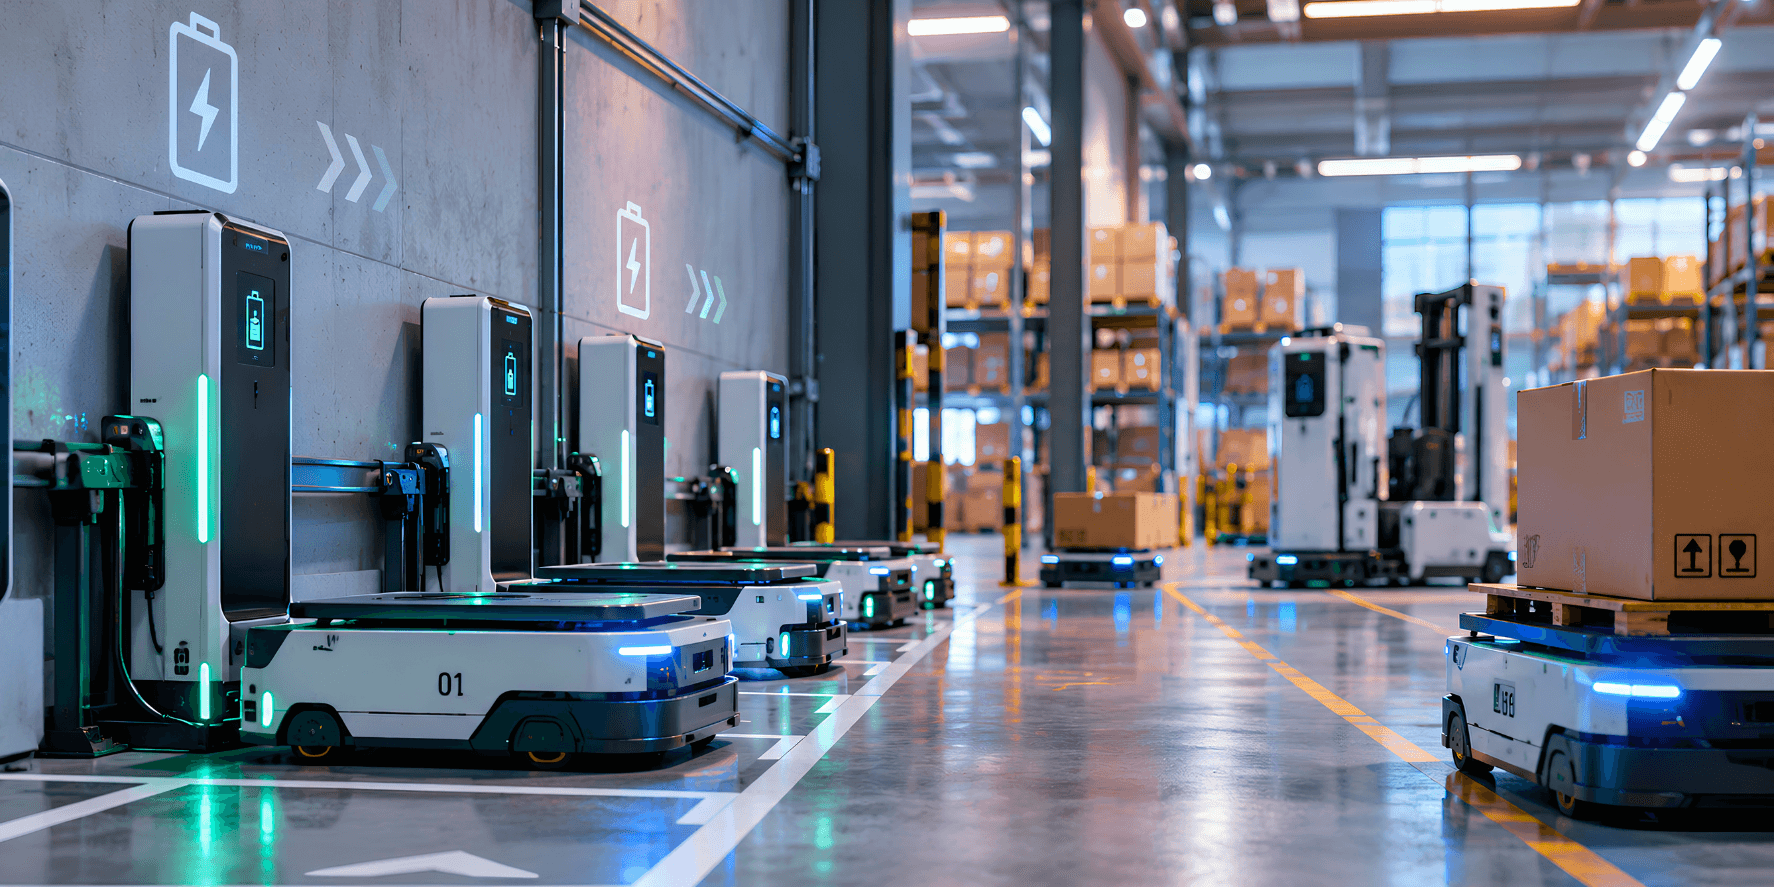
Charging is usually treated as an electrical question and handed to an electrician. The harder question is how much productive floor space the dock bank consumes, and how much of the fleet sits parked when throughput pea
Robot Charging Infrastructure: Battery Strategy, Opportunity Charging, and Floor Space Planning
Charging is usually the last line on an automation plan and the first thing to cause trouble after go-live. It gets handed to an electrician, who answers the question that was asked: can we get power to that wall? The answer is almost always yes.
The question that decides the outcome is different. How much productive floor space will the charging layout consume, and how much of the fleet will be parked when throughput peaks? Charging infrastructure for mobile robots should be sized from a charge budget rather than from a robot count. A charge budget is the ratio of charging time to running time across a full operating day, applied to the busiest hour instead of the daily average. Once that ratio is known, the strategy decision follows, and the floor space cost follows from the strategy.
Why Charging Gets Planned Last
Most vendor quotes include a charging dock, so charging reads as solved. The dock is a small object, roughly the size of a filing cabinet lying down, and it is easy to assume it will fit somewhere. In a working building, somewhere is already occupied.
The constraints that govern robot selection in the first place, the ones that mean racking, aisle widths, and mezzanines limit your automation options, also govern where a dock bank can go. A brownfield warehouse retrofit rarely has a convenient empty wall near the pick face.
Charging also tends to be modeled at pilot scale, where three robots share one dock and nothing queues. That model does not survive growth, which is why charging is among the first things to break when a fleet scales from five robots to fifty.
Decision One: Build the Charge Budget Before You Size the Fleet
Published specifications give a usable starting point. A common tote class autonomous mobile robot carries a 1.63 kWh lithium pack, runs about 13 hours at maximum payload, and reaches 90 percent in roughly 52 minutes on its matched dock. A pallet handling machine carries about 4.2 kWh, runs about 10 hours from 90 to 10 percent, and returns to 90 percent in about an hour.
Table 1: Charge budget reference points by robot class
| Red Flag | Why It Matters to Automation | What to Measure | What to Watch For |
|---|---|---|---|
| Missing load application drawings | No documented basis for beam elevations or capacity | Original rack drawings and load plaques | Reconfiguration needs engineering from scratch |
| Beam deflection or leaning uprights | Placement sensors rely on predictable rack geometry | Deflection against L/180, and upright plumb | Automated systems often specify a tighter L/240 |
| Rack damage at aisle entries | Reduces true clear width, marks repeat impact points | Clear width at the narrowest point of every aisle | Column protectors reduce the usable dimension further |
| Mezzanine designed for static storage | Robot wheel loading is concentrated and repetitive | Design live load and deck robot load rating | Code impact factors of 30 percent or more |
| Single vertical transport point | A whole level's volume passes through one device | Cycle time and units per hour at peak | A bottleneck no fleet size can relieve |
| Unknown floor flatness | Requirements are set per manufacturer, not by standard | Survey against the vendor's written requirement | A generic industrial specification proves nothing |
Figures are published manufacturer specifications for representative machines. Ratios are calculated from them and will vary with duty cycle, payload, and travel distance.
A 1:10 ratio looks generous. On paper one dock could supply ten robots. In practice it cannot, for three reasons that compound.
Demand arrives in waves rather than queues, because robots deployed together deplete together. Rated runtime assumes a new pack, and both classes above are rated for roughly 3,000 cycles before capacity falls below 80 percent, so a fleet sized on day one energy runs short long before the batteries are replaced. And the trip to the dock is unproductive travel that grows as the bank moves further from the work.
A defensible planning ratio sits closer to one dock per four to six robots for a single shift operation, and tighter than that across multiple shifts. The exact number should come from a measured duty cycle, not a spreadsheet assumption.
Decision Two: Match the Strategy to the Duty Cycle
Three approaches are in general use, and they trade against each other rather than ranking.
Table 2: Charging strategies compared
| Approach | How it works | Effect on fleet availability | Effect on floor space | Best fit |
|---|---|---|---|---|
| Opportunity charging | Short top-ups during natural gaps in the work, often a few minutes at a time | Highest. Robots rarely leave rotation | Highest cost. Docks must sit near the work, which is the most valuable floor area | Multi-shift operations with irregular idle gaps |
| Scheduled full cycle | Robots rotate out for a complete charge at set points in the day | Lower. A fixed share of the fleet is parked by design | Lowest cost. Docks can occupy a back wall or low value corner | Single shift operations with a predictable lull |
| Battery swap | Depleted packs are exchanged for charged ones in minutes | High, but depends on labor being present to swap | Moderate. Needs a swap area plus storage and charging for spare packs | High utilization operations that can staff the swap |
Availability and space effects are directional. The right choice depends on where idle time actually occurs on the operating day.
Battery chemistry decides whether opportunity charging is available at all. Lithium packs tolerate frequent partial charging and are commonly rated at 2,000 to 3,000 cycles at charge efficiency approaching 99 percent. Lead acid batteries prefer full uninterrupted cycles, typically deliver 1,000 to 1,500 cycles at roughly 80 percent efficiency, and conventionally need 8 to 10 hours of charging followed by 6 to 8 hours of cooling. Opportunity charging a lead acid pack shortens its life rather than extending the shift.
Mixed fleets make this a scheduling problem as well as a hardware one, which is where fleet management software earns its place. Charge scheduling that understands both chemistry and order release is the difference between a dock bank that smooths demand and one that creates a queue.
Decision Three: Count the Floor Space the Docks Actually Need
This is where charging plans go wrong most often. The dock is small. The envelope around it is not.
Published clearance guidance for one tote class charging station calls for about 2.8 meters of clear approach in front of the dock, 0.8 meters between adjacent stations, and side clearance of 0.7 meters on one side and 0.35 meters on the other. The dock itself is only about 0.24 meters deep and 0.62 meters wide.
Table 3: Floor area consumed by a charging bank
| Docks in the bank | Bank width | Approach depth | Total floor area | Roughly equivalent to |
|---|---|---|---|---|
| 1 | 1.7 m (5.5 ft) | 2.8 m (9.2 ft) | 4.7 sq m (50 sq ft) | 3 to 4 floor pallet positions |
| 2 | 3.1 m (10.1 ft) | 2.8 m (9.2 ft) | 8.7 sq m (93 sq ft) | 7 floor pallet positions |
| 4 | 5.9 m (19.5 ft) | 2.8 m (9.2 ft) | 16.6 sq m (179 sq ft) | 13 floor pallet positions |
| 6 | 8.8 m (28.8 ft) | 2.8 m (9.2 ft) | 24.6 sq m (264 sq ft) | 20 floor pallet positions |
| 8 | 11.6 m (38.1 ft) | 2.8 m (9.2 ft) | 32.5 sq m (350 sq ft) | 26 floor pallet positions |
Areas are calculated from one manufacturer's published clearance figures at standard settings and compared against 48 by 40 inch pallet footprints before aisle access. Clearances are vendor specific and are not standardized across the industry.
Eight docks is not unusual for a fleet in the thirties, and 350 square feet is not a rounding error in a building where every square foot was already assigned. A charging robot has also not left the floor. It holds that approach envelope for the duration, and in a narrow aisle layout the envelope can block traffic the throughput model assumed was free.
Placement then works against itself. Opportunity charging only delivers its availability advantage if docks sit close to where robots naturally pause: the pick face, the induct, outbound staging. Those are the most contested parts of the floor. Push the docks to a back wall and the space is cheaper, but every charge event now carries a round trip that was not in the model.
Decision Four: Confirm the Supply Matches the Charge Rate You Assumed
Quoted charge times assume the dock is receiving the input it was designed for. One common 48 volt dock delivers up to 40 amps on a 240 volt supply and only 20 amps on a 120 volt supply. Half the current means roughly double the charge time, which quietly doubles dock occupancy and can invalidate the entire charge budget.
Circuit sizing matters too. Under the National Electrical Code, a load expected to run at maximum current for three hours or more is a continuous load, and articles 210.19(A)(1) and 210.20(A) require conductors and overcurrent protection rated at 125 percent of it. A dock bank running back to back sessions through a shift reaches that threshold easily.
Knowing which safety rules apply matters as well. OSHA 29 CFR 1910.178(g) governs charging storage batteries for powered industrial trucks, requiring designated charging areas, spill neutralization, fire protection, and ventilation for gassing batteries. It is written for forklifts and references ANSI B56.1. A sealed lithium pack does not gas, and mobile robots fall under the ANSI/A3 R15.08 series instead. The risk runs both ways: budgeting for a ventilated battery room nobody needs, or assuming nothing applies on a site that runs lead acid forklifts alongside lithium robots and so carries both sets.
How to Size Charging Before You Commit
Table 4: Pre-deployment charging audit
| What to confirm | Why it matters | Where the answer comes from |
|---|---|---|
| Peak hour robot utilization, not daily average | Dock demand is set by the busiest window | Order profile and WMS release data |
| Charge to run ratio for the specific robot and payload | Published runtime assumes rated conditions | Manufacturer specification, verified in a pilot |
| Battery chemistry and cycle rating | Decides whether opportunity charging is viable | Manufacturer specification |
| Supply voltage available at the intended dock location | Charge time can double on a 120 volt supply | Electrical drawings and a site walk |
| Circuit capacity and panel headroom | Continuous load sizing may require new circuits | Licensed electrician |
| Clear floor area including approach envelope | The envelope, not the dock, is the real footprint | Vendor clearance data and a measured layout |
| Capacity at 80 percent of rated battery life | Prevents a fleet that performs only while new | Cycle rating plus planned service life |
Complete this before fleet size is fixed. Every row that is estimated rather than measured becomes a risk carried into go-live.
Most of these answers exist only once robots are moving in the building. That is the argument for measuring duty cycle in a bounded proof-of-concept program before committing to a dock count, and for carrying charging infrastructure as a capital line in the warehouse automation ROI case rather than an installation detail.
Planning Charging With Robotech Pros
Robotech Pros works with operators on the layout and infrastructure questions that decide whether a fleet performs as modeled. If you are evaluating autonomous mobile robots or AGVs for an existing facility, we can help map duty cycle, charging strategy, and dock placement against the floor space you have, so charging capacity is settled during design rather than discovered after go-live.
Related resources
How Many AMRs Do You Actually Need? A Guide to Throughput Modeling
Most AMR fleet sizes are guessed before anyone counts the moves. This guide walks through the four-step throughput model that replaces the guess, and explains why doubling throughput takes more than double the robots.
How Racking, Aisle Widths, and Mezzanines Limit Your Automation Options
Most automation shortlists are decided by the building, not the vendor. A practical look at how rack configuration, clear aisle width, and mezzanine design rule options in or out, and what to measure before you invite an
Scaling From 5 Robots to 50: What Breaks When Your Fleet Grows
What breaks when a warehouse robot fleet grows from 5 to 50, and the traffic, charging, network, and integration checks to complete before you expand.